Executive Summits · by the Future of Manufacturing Alliance
Dust Collection & Industrial Ventilation Summit for Manufacturing Plants
Meet the plant leaders who can see the haze from the mezzanine.
Each summit is capped at 20 sponsors. Talk to Joe before it fills.
Who’s coming so far
21 manufacturers have confirmed they will send people. The target is 100+ plant leaders in the room by each summit.
- Honda
- GE Aerospace
- General Motors
- Stellantis / Jeep
- Procter & Gamble
- Cleveland-Cliffs
- Whirlpool
- Goodyear Tire & Rubber
- Parker Hannifin
- Swagelok
- Crown Equipment
- Lincoln Electric
- Sherwin-Williams
- + 8 very large manufacturers, not named at their request
Two days with EHS, plant engineering and maintenance leaders from Midwest manufacturers dealing with weld fume, combustible dust, exposure limits and make-up air costs. Pre-scheduled 1-on-1 meetings. No expo hall.
The people who sign the PO for dust collection projects.
Invited from plants across Ohio, Michigan, Indiana, Pennsylvania and Kentucky. Every delegate is screened by title and plant.
1,470plant leaders from 495 manufacturers have come to past FMA summits.1,033 of them pick the vendor, own the budget or sign off.
Who decides a plant purchase, and how many came
- Step 1287Find the problem, write the specEnergy Engineer, Facilities Engineer, Environmental Engineer
- Step 2560Pick the vendorFacilities Manager, Environmental Manager, Energy Manager
- Step 3337Own the budgetDirector of Engineering, Director of Operations, Director of Manufacturing
- Step 4136Sign offPlant Manager, General Manager, President
Who we invite to this summit
Each title, and what that person owns.
- EHS ManagerExposure and dust hazards
- Plant Engineering DirectorSpecifies the system
- Maintenance ManagerFilters, fans, pulse air
- Plant ManagerSigns off on capex
- Facilities ManagerMake-up air and heat
Where past delegates worked
Plant leaders at past FMA summits, by industry.
Industries we are inviting to this summit: Metals and fabrication (weld fume, grinding) · Automotive and parts (Ohio, Michigan, Indiana) · Food and grain (combustible dust) · Wood and building products (sawdust, sanding) · Plastics and chemicals (powders, mist).
Counts are past FMA delegates, each counted once. They show who this audience is; they are not 2027 attendees.
Past speakers and delegates, by industry
Food and beverage
12 speakers · 161 delegates


Automotive
10 speakers · 192 delegates


Machinery, equipment and electronics
7 speakers · 209 delegates

Chemicals, plastics and rubber
6 speakers · 120 delegates
Steel and metals
2 speakers · 82 delegates
Aerospace, pharma, building and consumer products
29 speakers · 667 delegates




They came back.
Past FMA sponsors, and how many summits each one sponsored, from the printed programs.
- 2CamfilAir filters · 2 summits
- 18US LED18 summits
- 17Kaeser Compressors17 summits
- 14Covanta14 summits
- 14Solution Dynamics14 summits
- 10Advanced Power Technologies10 summits
- 8Smardt Chiller Group8 summits
- 7BASF7 summits
- 7EQUIDEX Energy7 summits
- 7LG Electronics7 summits
- 6AgriPower6 summits
- 6Greenstar Recycling6 summits
See the other 102 companies that sponsored two or more FMA summits
3M 2 · Acuity Brands 4 · Advanced Green Technologies 3 · Advantix Systems 8 · AERCO International 5 · Air Balance 2 · AmbiRad 3 · Ameresco 2 · Armstrong Fluid Technology 5 · Badger Meter 2 · Be Power Tech 2 · Bio-Reaction Industries 2 · BLUEFIN 4 · Bosch Thermotechnology 2 · Burns & McDonnell Engineering 3 · Capstone Turbine 2 · Chelsea Group 2 · Cleaver-Brooks 4 · ConDex Energy 2 · Constellation Energy 5 · Control Instruments 2 · CopperTree Analytics 3 · Cushman & Wakefield 2 · Cypress Envirosystems 5 · Doosan Fuel Cell America 3 · DTE Energy Services 2 · Dyson 4 · Eaton 3 · EcoSafe Zero Waste 2 · EDF Renewable Energy 2 · Edison Energy 2 · Emerson Climate Technologies 2 · Energy Management Systems 4 · Energy Source 2 · EnerNOC 2 · Enertech Global 2 · EnterSolar 2 · Environmental Resources Management 2 · ERS International 3 · ETwater Systems 2 · Every Watt Matters 2 · Eye Lighting International 3 · Facility Solutions Group 2 · FacilityConneX 2 · Fellon-McCord & Associates 3 · GDF SUEZ Energy NA 2 · GE Distributed Power 2 · GE Solar 2 · Gexpro 3 · GI Energy 2 · Green Ballast 2 · Greenworks Energy Solutions 3 · Harris Lighting 2 · Heritage Interactive Services 2 · Hurst Boiler & Welding Co. 2 · IBM 4 · ICETEC Energy Services 2 · ICONICS 3 · Invensys Operations Management 2 · JLL 4 · Jorgensen Facilities Services 5 · K+S Services 2 · KDC Solar 2 · KERAMIDA 2 · Knauf Insulation 2 · KVAR Energy Savings 3 · LEDtronics 2 · Lutron Electronics Co. 3 · MaxLite 2 · MCEnergy 2 · MEP Associates 2 · MPC Energy 5 · Munters 2 · Newton Distributing Company 2 · Nortec 3 · North America Power Partners 2 · North American Roofing 2 · OAKLEAF 4 · Optimum Energy 2 · Orion Energy Systems 2 · OSRAM SYLVANIA 5 · Pfister Energy 2 · PowerSecure 5 · Rinnai America 2 · Rockwell Automation 2 · ROXUL 2 · Rubicon Global 2 · SAP America 2 · Schneider Electric 6 · Shaw Environmental & Infrastructure 5 · Sloan 2 · Solar UV Solutions 3 · Solatube International 3 · Steril-Aire 2 · Synergy Investment 6 · The Dow Chemical Company 2 · Thermal Energy International 3 · Trane 2 · Tremco Roofing and Building Maintenance 2 · Viridity Energy 2 · Wahaso - Water Harvesting Solutions 2 · Zurn Industries 2
In writing, from past delegates.
Their words, not ours.
“Every year we are able to find new partners to develop breakthrough projects”
 Breitner MarczewskiDirector of Energy Engineering, General Motors
Read the whole quote
“FMA Summit has been a very friendly business event for General Motors. Every year we are able to find new partners to develop breakthrough projects”
“We will be partnering with a couple of the presenters at the Summit”
Read the whole quote
“…The expertise represented at this Summit (solar, lighting, etc.) was impressive and very informative. We will be partnering with a couple of the presenters at the Summit…”
 Scott CullenAmericas Environmental Compliance Manager, Bostik
“…full of opportunities to network with vendors I was interested in”
Read the whole quote
“I found the experience well organized and full of opportunities to network with vendors I was interested in.”
 Warren VoughtCorporate Facilities Manager, Archer Daniels Midland
“…so we can learn more about what each company has to offer”
Read the whole quote
“The presenters were very knowledgeable and did a great job of communicating during the one on one time during breaks. I look forward to the site visits so we can learn more about what each company has to offer.”
 John ShewmakerFacility Maintenance Manager, Hitachi Automotive Systems
See 8 moreShow fewer
“I am always skeptical with conferences whether they will be worth my time. This Summit was a very good blend and balance of solutions and testimonials. I will recommend this seminar to others in my company…”
 Larry GlaserAVP, Director of Operations Support, OSI Industries
“…Enjoyed the Summit and met some good contacts.”
 Russ DelozierDirector of Sustainability, J+J Flooring Group
“Great Summit to attend and see the diversity of industry and government. Several vendors presented new ideas to problems we all face in the industry.”
 Ed HagerstromDirector EHS, Refresco Beverages US Inc.
“Excellent set of presenters on a wide range of subjects, lots of new and forward thinking. Great networking with small groups- startup dinners and circulation times.”
 John DeVinneySenior Project Manager, Perdue Farms
“I’ve been to a lot of conferences and I found the FMA sessions to be excellent, engaging and interesting. I think it had some of the best speakers I’ve ever seen in a conference I’ve been to. I certainly liked the format, the 20 minutes sessions, so you can get the top level ideas or thoughts without having to hear in infinite detail. The format is well structured, the speakers were really, really good and I would highly recommend this conference to anybody in this field.”
 Brendan SullivanExecutive Director, Facilities, Estée Lauder
“The Summit was truly ‘eye-opening’. I got an excellent sense of momentum building for companies and institutions making significant changes for the future. Woe betide those organizations who turn a blind eye to the need and benefits of changing how they manage and operate their facilities.”
 Chris WendtFacilities Manager, Standard Motor Products, Inc.
“As a global leader, it’s extremely important for me to stay current on technological advances. The FMA Summit brought current advances and best practices to me in an efficient 1.5 day event”
 Maria WatsonSr. Manager Global Energy, Pall Corporation
“The FMA Energy and Sustainability Summit provides valuable insight into where leaders in various industries are finding success in systems and processes that drive overall efficiencies and organizational sustainment.”
 Brian SkrobarcekCorporate Director of Environmental Affairs, StandardAero
What sponsors closed, and what buyers said.
Past sponsors on the business that came from an FMA introduction, and past buyers on the vendors they met there.
Set up Wednesday. Two full days of meetings. Home Friday afternoon.
Same schedule in Columbus and Detroit.
- Wednesday afternoonSponsors set up their exhibits. Everyone checks in.
- ThursdayThe full day: plant case studies, booked 1-on-1s, the reception and dinner.
- FridayMorning case studies, more 1-on-1s, closing lunch. On the road by mid-afternoon.
The hour-by-hour plan and the venues
| Time | Wednesday | Thursday | Friday |
|---|---|---|---|
| 7:00 AM | Breakfast at your company table | Breakfast at your company table | |
| 8:00–10:00 AM | Plant case studies | Plant case studies | |
| 10:00 AM | Coffee and shop talk in the exhibit room | Pre-booked 20-minute 1-on-1s at your table | |
| 11:00 AM | Plant case studies | Plant case studies | |
| 12:00 PM | Lunch with your booked 1-on-1 meetings | Closing lunch with your booked 1-on-1 meetings | |
| 1:00 PM | Plant case studies | Plant case studies, then head home | |
| 2:00 PM | Sponsor setup and check-in | Pre-booked 20-minute 1-on-1s at your table | |
| 3:00 PM | Sponsor setup and check-in | Coffee and shop talk in the exhibit room | |
| 3:30 PM | Sponsor setup and check-in | Plant case studies | |
| 5:00–7:00 PM | Sponsor setup and check-in | Reception and dinner, with more 1-on-1s |
The full package's 15 pre-booked 20-minute 1-on-1s run Thursday and Friday: in the meeting blocks above, at lunch, and at the reception. Each is with a plant leader who asked to meet you, at your company table. You get your meeting schedule before you arrive, and the delegate list, with names, titles and companies, 30 days before the summit.


Venue photos via Wikimedia Commons: Hilton Columbus Downtown by Ɱ (CC BY-SA 4.0); Renaissance Center by Crisco 1492 (public domain).
The program: plant leaders come to hear how other plants fixed it.
The program is built from projects plants actually finished, presented by the plant and the company that did the work. Every dust collection and ventilation category has room for more. If you've solved a problem like these, your story belongs on this program.
-
Combustible dust safetyInvited
Designing for combustible powders from day one: 1440 Foods' expansion in Jeffersonville, Indiana
A cartridge collector with custom capture hoods and stainless ductwork, protected by explosion vents, an explosion-rated rotary airlock and a Vigiflap explosion isolation valve; the ingredients tested at Kst 87 to 145 bar-m/s, equipment arrived in about eight weeks and the project was completed toward the end of 2025. No performance figures are given (as reported by Baghouse.com, with an ACT collector).
The problem: A plant expansion added powder dumping, blending, sifting and bar-kitchen mixing that released visible dust, and lab tests showed the ingredients were combustible, so the dust hazard analysis required both source capture and explosion protection.
Published result: A cartridge collector with custom capture hoods and stainless ductwork, protected by explosion vents, an explosion-rated rotary airlock and a Vigiflap explosion isolation valve; the ingredients tested at Kst 87 to 145 bar-m/s, equipment arrived in about eight weeks and the project was completed toward the end of 2025. No performance figures are given (as reported by Baghouse.com, with an ACT collector).
Invited: Baghouse.com and ACT Dust Collectors, with 1440 Foods · Read the published case
-
Ventilation & make-up airInvited
Keeping a 165,000 sq ft medical-grade plant addition positively pressurized in Hazleton, Pennsylvania
Four 100,000 CFM variable-volume direct-fired make-up air units against a calculated need of about 265,000 CFM, so three run below full capacity with one on standby, controlled to measured space pressure through a Lynxspring JENEsys Edge 514 controller; the case history reports savings in gas and electricity costs but gives no figures (as reported by AbsolutAire and Lynxspring; customer not named).
The problem: A new 95-foot-high plant addition making medical-grade absorbent material had to stay positively pressurized to keep contaminants out while exhaust fans cycled and overhead doors opened and closed.
Published result: Four 100,000 CFM variable-volume direct-fired make-up air units against a calculated need of about 265,000 CFM, so three run below full capacity with one on standby, controlled to measured space pressure through a Lynxspring JENEsys Edge 514 controller; the case history reports savings in gas and electricity costs but gives no figures (as reported by AbsolutAire and Lynxspring; customer not named).
Invited: AbsolutAire, with Lynxspring · Read the published case
-
Dust collectorsInvited
How a Midwest steel plant cut airborne dust 90% at its hopper-loading station
An engineered cartridge dust collector with a HEPA stage, a reconfigured existing collector on the conveying line and a bin vent on the final product bins: the Plant Manager confirmed a 90% reduction in airborne dust, clean-up was cut by over 90%, daily cleaning of two to three hours became a biweekly routine, and workers no longer need protective masks (measured by the plant; as reported by Benetech; customer not named).
The problem: Front-end loaders filling hoppers with calcium aluminate and limestone threw off dust that an undersized collector could not handle, and that collector exhausted air back into the building above the permissible limit for recycled air.
Published result: An engineered cartridge dust collector with a HEPA stage, a reconfigured existing collector on the conveying line and a bin vent on the final product bins: the Plant Manager confirmed a 90% reduction in airborne dust, clean-up was cut by over 90%, daily cleaning of two to three hours became a biweekly routine, and workers no longer need protective masks (measured by the plant; as reported by Benetech; customer not named).
Invited: Benetech · Read the published case
See all 8 stories, in 4 categories, and how a session runs
- 1The problemWhat was happening at the plant.
- 2The costEnergy, maintenance, downtime or lost output.
- 3The decisionThe options they weighed, and why this one.
- 4The workWhat changed, how long it took, what went wrong.
- 5The resultsMeasured before and after. Achieved, estimated or identified, said plainly.
- 6The lessonsWhat another plant should check first.
-
Dust collectors
3 stories invited · 1 open slot-
Invited
How a Midwest steel plant cut airborne dust 90% at its hopper-loading station
An engineered cartridge dust collector with a HEPA stage, a reconfigured existing collector on the conveying line and a bin vent on the final product bins: the Plant Manager confirmed a 90% reduction in airborne dust, clean-up was cut by over 90%, daily cleaning of two to three hours became a biweekly routine, and workers no longer need protective masks (measured by the plant; as reported by Benetech; customer not named).
The problem: Front-end loaders filling hoppers with calcium aluminate and limestone threw off dust that an undersized collector could not handle, and that collector exhausted air back into the building above the permissible limit for recycled air.
Published result: An engineered cartridge dust collector with a HEPA stage, a reconfigured existing collector on the conveying line and a bin vent on the final product bins: the Plant Manager confirmed a 90% reduction in airborne dust, clean-up was cut by over 90%, daily cleaning of two to three hours became a biweekly routine, and workers no longer need protective masks (measured by the plant; as reported by Benetech; customer not named).
Invited: Benetech · Read the published case
-
Invited
Nine gypsum plants, one dust-collection playbook: USG's audits from River Rouge, Michigan to Danville, Pennsylvania
Plant-by-plant inspections, training and redesigns: at River Rouge, Michigan two idle collectors were repurposed and a process baghouse was re-ducted and converted to pleated filters; at Walworth, Wisconsin four baghouse systems were reviewed and redesigned; at Danville, Pennsylvania new cages were recommended for every baghouse; at Fort Dodge the fix included adding a cyclone and switching from timer cleaning to clean-on-demand. No savings figures are given and the page is undated (as reported by Baghouse.com).
The problem: Across USG's wallboard and ceiling plants, collectors ran on timers around the clock, pressure gauges were unreliable, ductwork no longer matched the process, and at Fort Dodge, Iowa a baghouse burned through hundreds of filters at a cost running into the hundreds of thousands of dollars.
Published result: Plant-by-plant inspections, training and redesigns: at River Rouge, Michigan two idle collectors were repurposed and a process baghouse was re-ducted and converted to pleated filters; at Walworth, Wisconsin four baghouse systems were reviewed and redesigned; at Danville, Pennsylvania new cages were recommended for every baghouse; at Fort Dodge the fix included adding a cyclone and switching from timer cleaning to clean-on-demand. No savings figures are given and the page is undated (as reported by Baghouse.com).
Invited: Baghouse.com, with USG · Read the published case
-
Invited
From quarterly inspections to sensors: a mid-South minerals plant's 23 dust collectors
A six-month trial of Donaldson's iCue connected monitoring traced the back-up through pressure-drop data and fixed it with a fan-cycle change; the plant plans to monitor all 23 collectors and projects 75% less preventive-maintenance time, with an estimated nine-month return on the installation and first-year subscription (projected and estimated; page undated; as reported by Donaldson; customer not named).
The problem: Quarterly visual filter and solenoid checks took about 40 hours per collector a year and still missed problems, and one collector kept backing up with dust.
Published result: A six-month trial of Donaldson's iCue connected monitoring traced the back-up through pressure-drop data and fixed it with a fan-cycle change; the plant plans to monitor all 23 collectors and projects 75% less preventive-maintenance time, with an estimated nine-month return on the installation and first-year subscription (projected and estimated; page undated; as reported by Donaldson; customer not named).
Invited: Donaldson · Read the published case
- Open slot
Your customer's story goes here.
Solved a plant problem in this category? Propose it for the program.
-
-
Fume and mist extraction
1 story invited · 1 open slot-
Invited
How American Seating cleared weld fume from 18 booths without hot respirators
After testing a sample unit, the plant installed a Miller FILTAIR Centralized 12000 System with ZoneFlow extraction arms that capture fume at the source; installation took two days with two training sessions. No measured figures; the weld engineer calls it a huge improvement (as reported by Miller Electric).
The problem: Fifteen welders across eighteen manual booths were exposed to weld fume, the plant is not climate controlled and reaches above 100ºF in summer, so respirators were ruled out, and the old backdraft tables drew only about 200 cfm.
Published result: After testing a sample unit, the plant installed a Miller FILTAIR Centralized 12000 System with ZoneFlow extraction arms that capture fume at the source; installation took two days with two training sessions. No measured figures; the weld engineer calls it a huge improvement (as reported by Miller Electric).
Invited: Miller Electric, with American Seating · Read the published case
- Open slot
Your customer's story goes here.
Solved a plant problem in this category? Propose it for the program.
-
-
Combustible dust safety
1 story invited · 1 open slot-
Invited
Designing for combustible powders from day one: 1440 Foods' expansion in Jeffersonville, Indiana
A cartridge collector with custom capture hoods and stainless ductwork, protected by explosion vents, an explosion-rated rotary airlock and a Vigiflap explosion isolation valve; the ingredients tested at Kst 87 to 145 bar-m/s, equipment arrived in about eight weeks and the project was completed toward the end of 2025. No performance figures are given (as reported by Baghouse.com, with an ACT collector).
The problem: A plant expansion added powder dumping, blending, sifting and bar-kitchen mixing that released visible dust, and lab tests showed the ingredients were combustible, so the dust hazard analysis required both source capture and explosion protection.
Published result: A cartridge collector with custom capture hoods and stainless ductwork, protected by explosion vents, an explosion-rated rotary airlock and a Vigiflap explosion isolation valve; the ingredients tested at Kst 87 to 145 bar-m/s, equipment arrived in about eight weeks and the project was completed toward the end of 2025. No performance figures are given (as reported by Baghouse.com, with an ACT collector).
Invited: Baghouse.com and ACT Dust Collectors, with 1440 Foods · Read the published case
- Open slot
Your customer's story goes here.
Solved a plant problem in this category? Propose it for the program.
-
-
Ventilation & make-up air
3 stories invited · 1 open slot-
Invited
Keeping a 165,000 sq ft medical-grade plant addition positively pressurized in Hazleton, Pennsylvania
Four 100,000 CFM variable-volume direct-fired make-up air units against a calculated need of about 265,000 CFM, so three run below full capacity with one on standby, controlled to measured space pressure through a Lynxspring JENEsys Edge 514 controller; the case history reports savings in gas and electricity costs but gives no figures (as reported by AbsolutAire and Lynxspring; customer not named).
The problem: A new 95-foot-high plant addition making medical-grade absorbent material had to stay positively pressurized to keep contaminants out while exhaust fans cycled and overhead doors opened and closed.
Published result: Four 100,000 CFM variable-volume direct-fired make-up air units against a calculated need of about 265,000 CFM, so three run below full capacity with one on standby, controlled to measured space pressure through a Lynxspring JENEsys Edge 514 controller; the case history reports savings in gas and electricity costs but gives no figures (as reported by AbsolutAire and Lynxspring; customer not named).
Invited: AbsolutAire, with Lynxspring · Read the published case
-
Invited
Replacing an aging boiler and unit heaters at CJ Automotive in Indiana
Three Cambridge high-temperature heating and ventilation units (SA 250, S800 and S2200): estimated utility savings of 20%, the thermostat raised from 55°F to 68°F, boiler maintenance and repairs down by over 4 man hours a day, annual boiler inspection fees eliminated, and gas utility rebates (estimated; page undated; as reported by Cambridge Air Solutions).
The problem: Inefficient unit heaters and an aging boiler kept a 126,000 sq ft manufacturing and distribution facility uncomfortable while driving up winter utility bills, and the replacement had to go in without stopping the production line.
Published result: Three Cambridge high-temperature heating and ventilation units (SA 250, S800 and S2200): estimated utility savings of 20%, the thermostat raised from 55°F to 68°F, boiler maintenance and repairs down by over 4 man hours a day, annual boiler inspection fees eliminated, and gas utility rebates (estimated; page undated; as reported by Cambridge Air Solutions).
Invited: Cambridge Air Solutions, with CJ Automotive · Read the published case
-
Invited
Do big fans help in a hot steel plant? A field study in Baton Rouge, Louisiana
UC Berkeley researchers switched HVLS ceiling, wall and floor fans on and off over six weeks with 36 volunteer workers: fans reduced discomfort and perceived effort by the equivalent of a 9°F (5°C) drop in temperature, 79% of workers felt more effective with fans running, and core temperature, heart rate and sweat rate did not differ with or without fans (measured; research study funded by Big Ass Fans; as reported by the UC Berkeley Center for the Built Environment; plant not named).
The problem: Two adjacent steel manufacturing buildings in Baton Rouge have no air conditioning, and many guidelines still advise against using fans above 95°F.
Published result: UC Berkeley researchers switched HVLS ceiling, wall and floor fans on and off over six weeks with 36 volunteer workers: fans reduced discomfort and perceived effort by the equivalent of a 9°F (5°C) drop in temperature, 79% of workers felt more effective with fans running, and core temperature, heart rate and sweat rate did not differ with or without fans (measured; research study funded by Big Ass Fans; as reported by the UC Berkeley Center for the Built Environment; plant not named).
Invited: Big Ass Fans, with the UC Berkeley Center for the Built Environment · Read the published case
- Open slot
Your customer's story goes here.
Solved a plant problem in this category? Propose it for the program.
-
"Invited" means invited: none of these companies has confirmed. Results are as published by the supplier; we ask every presenter for dates, baseline costs and verified results before the program is final.
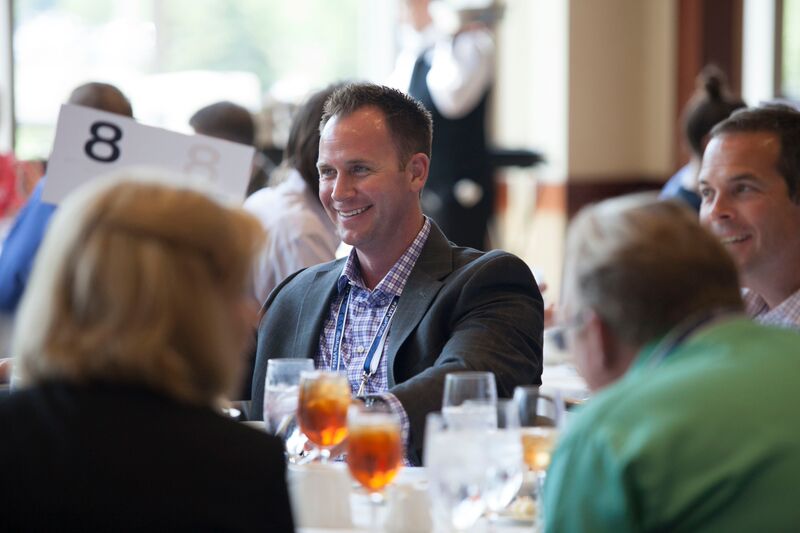
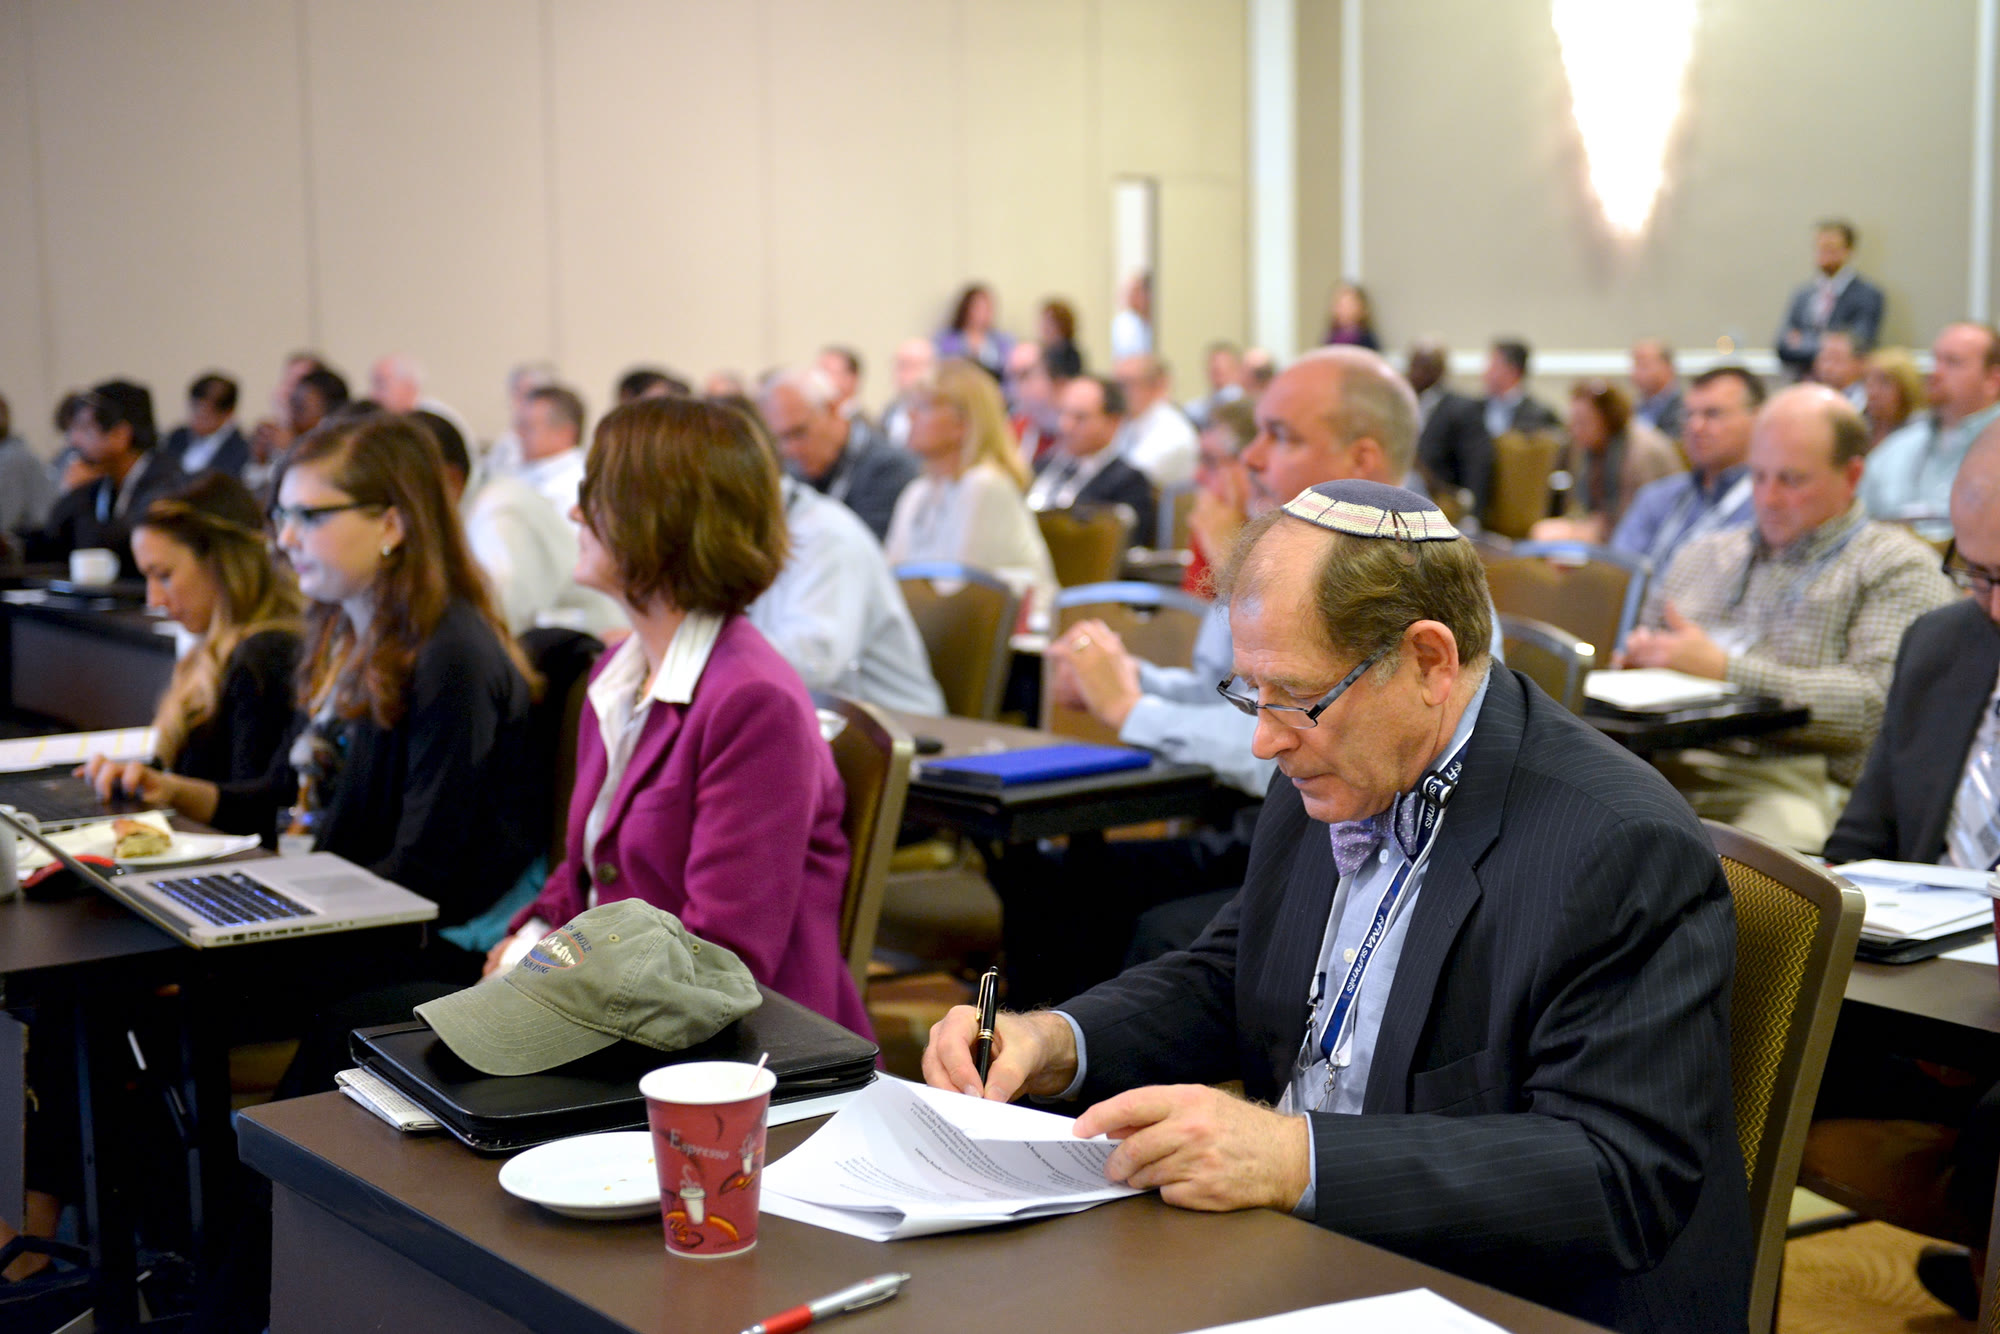
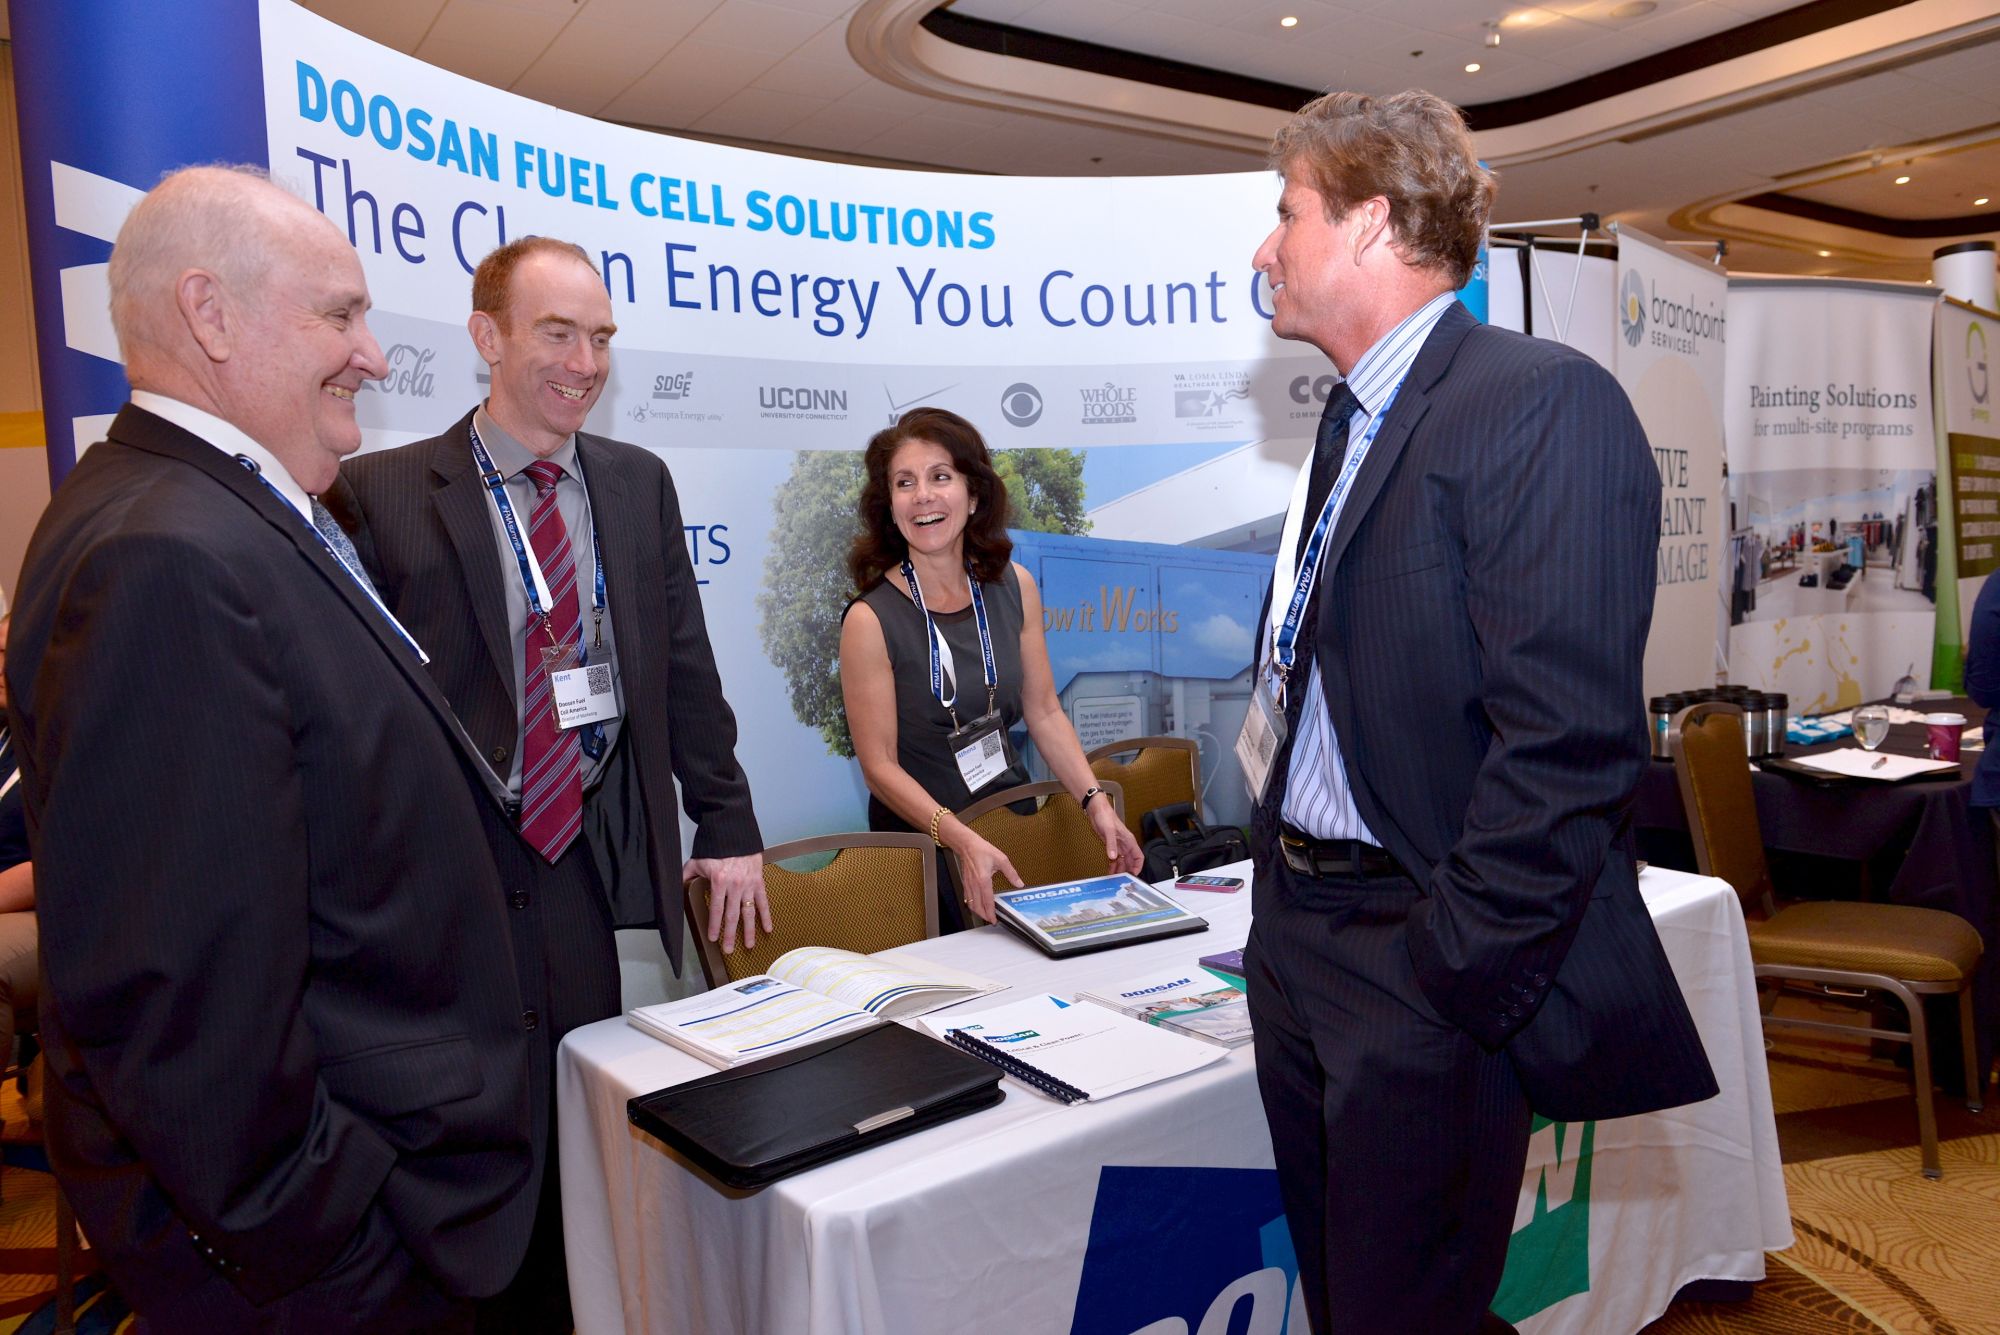
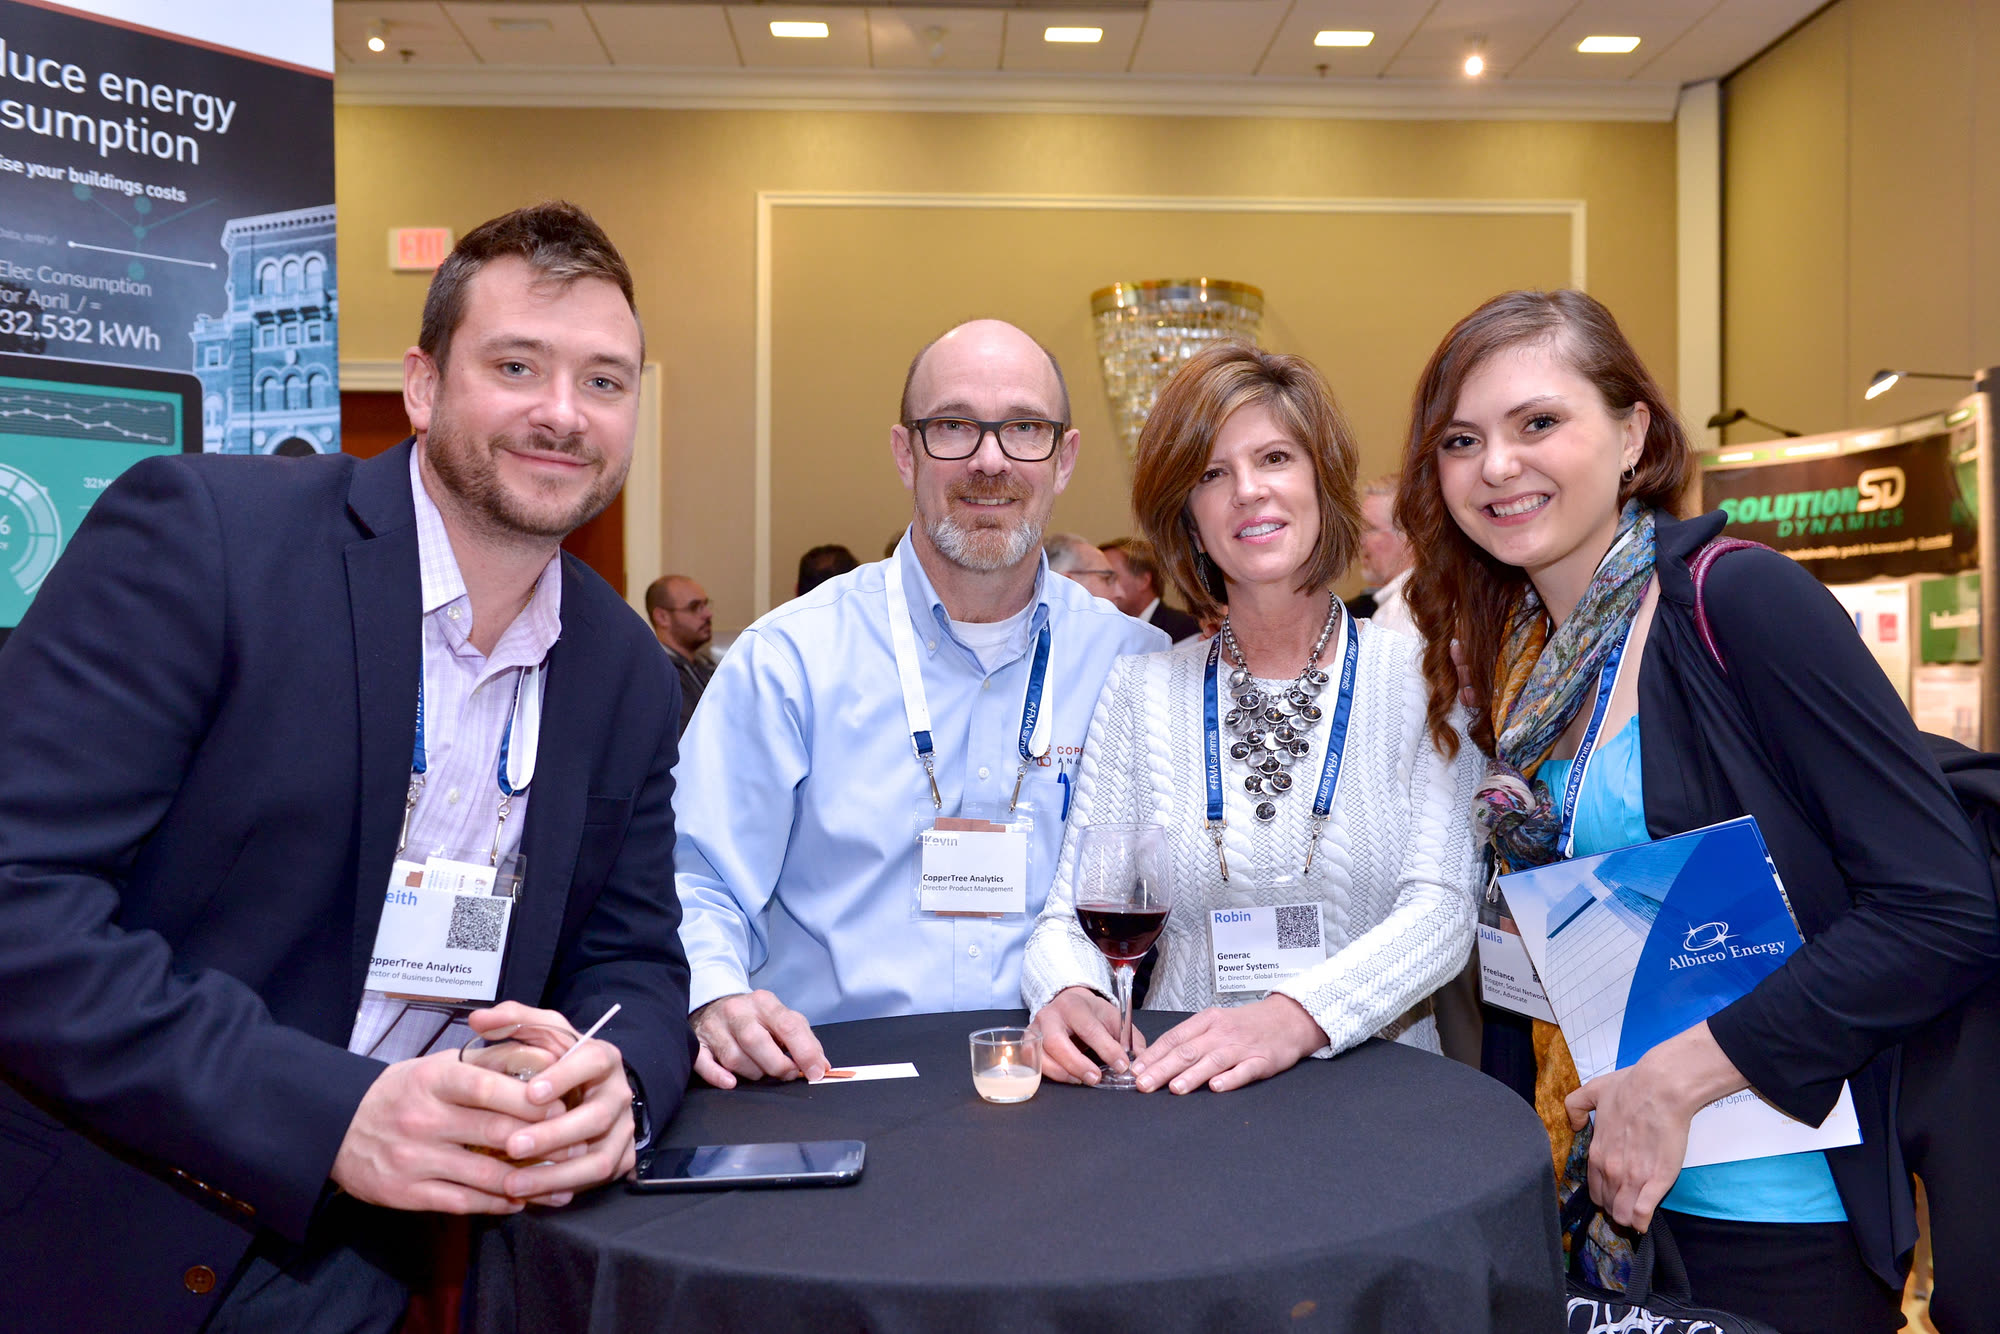
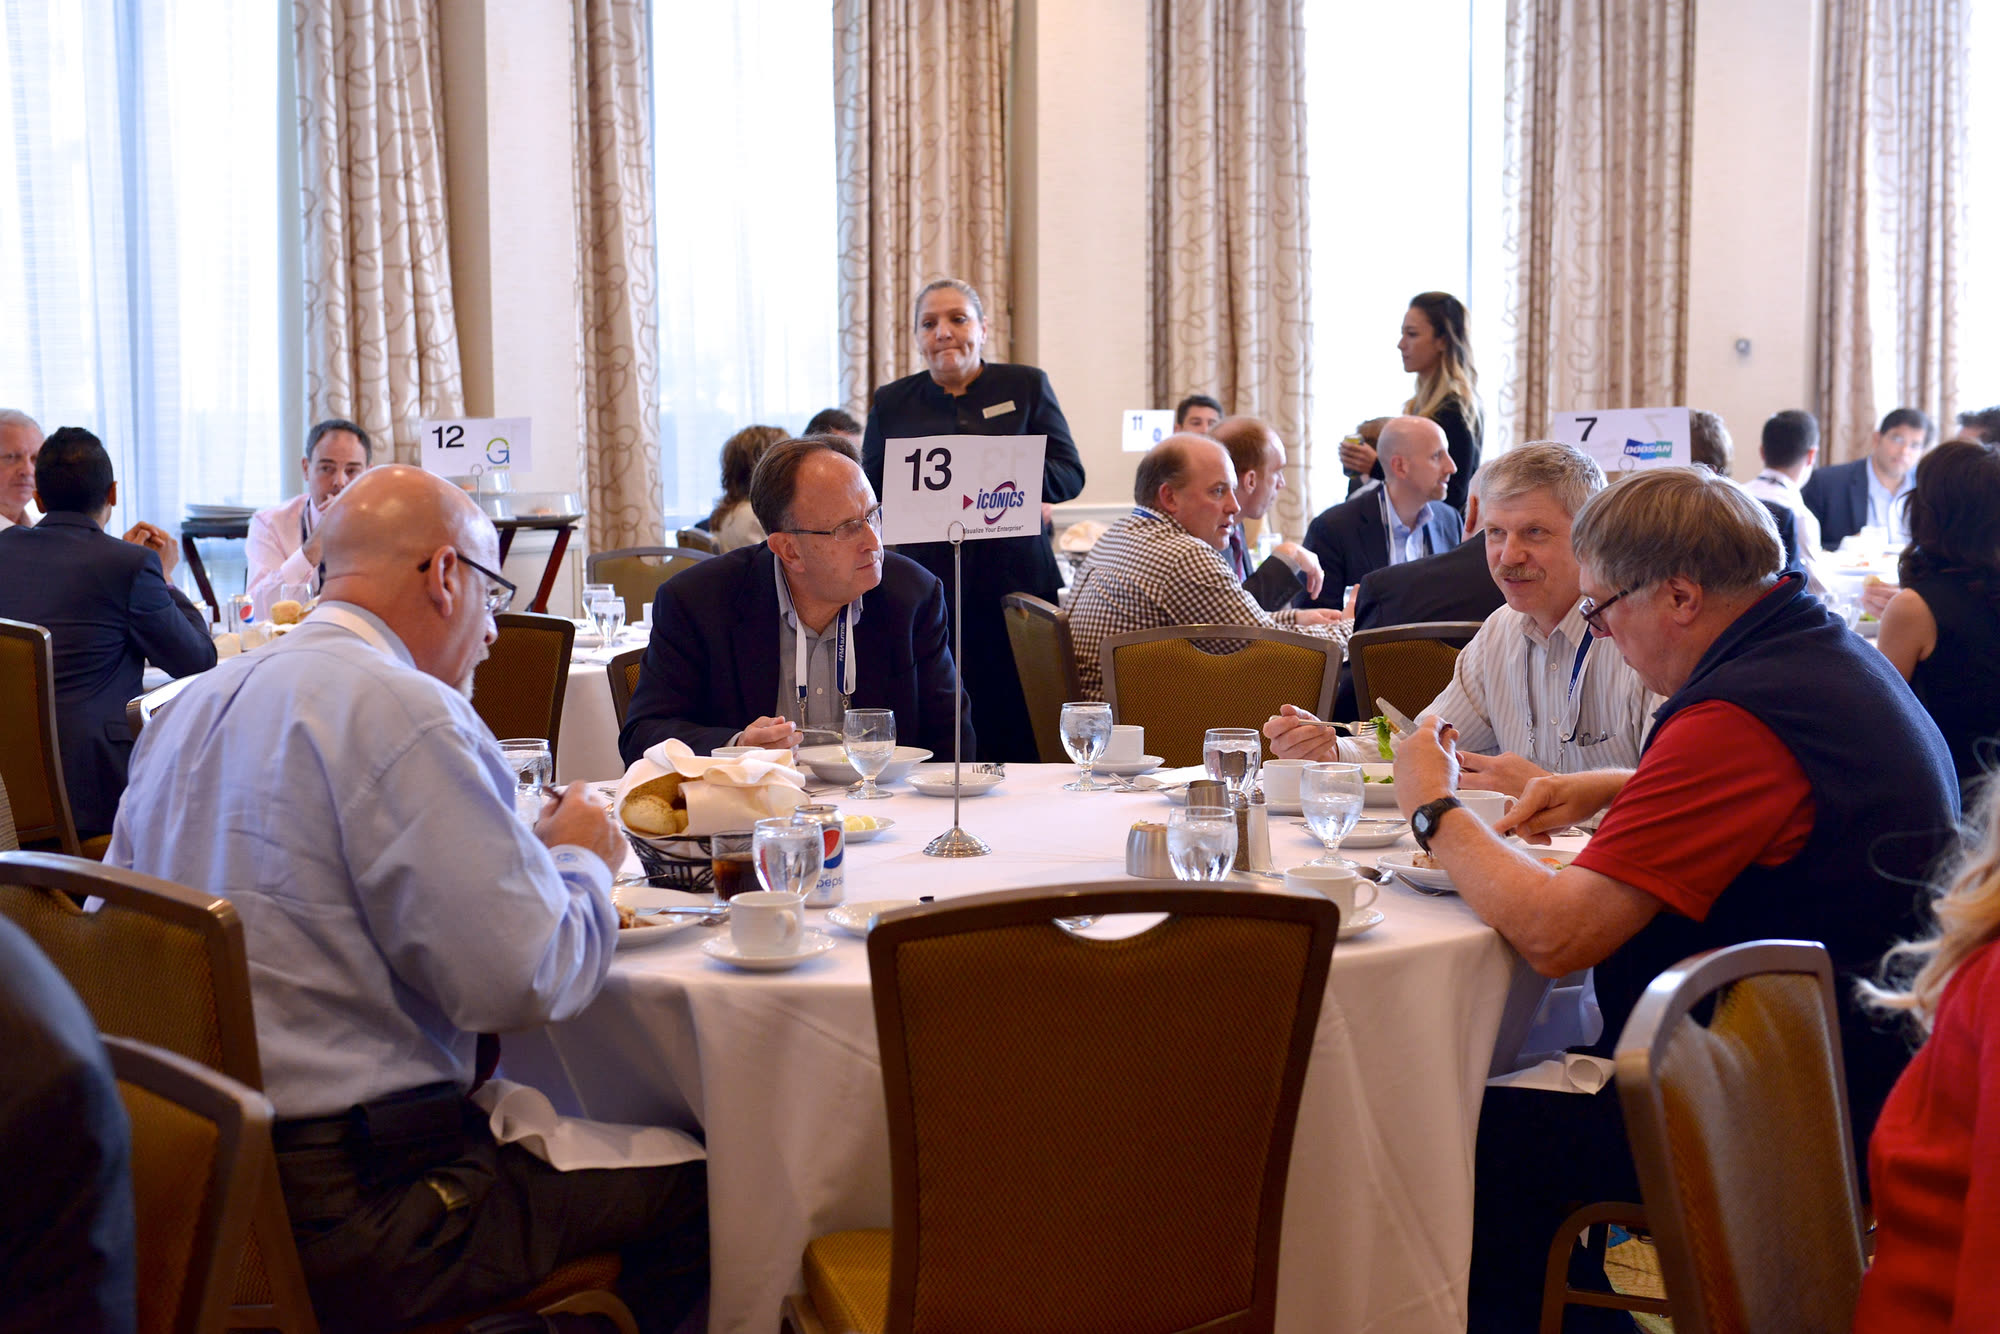
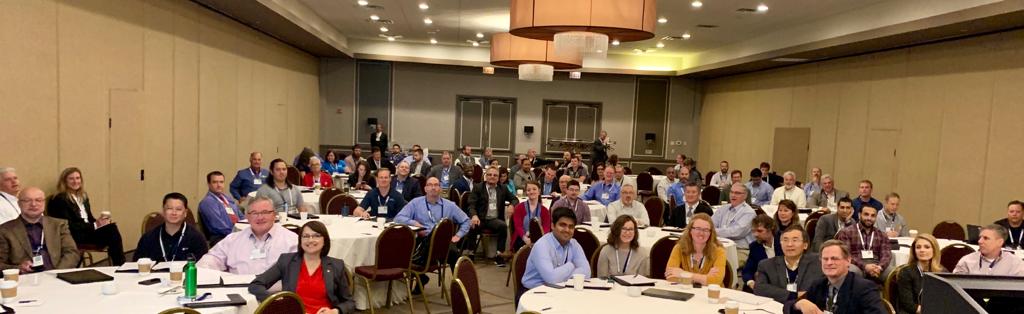
Real FMA Summit rooms. No stock photography.
Get in front of the decision makers, not the crowd.
Full package
- 15 guaranteed pre-scheduled meetings
- A 20-minute case-study session
- A fully furnished exhibit
- Your corporate dining table
- Three people at full access
Add meetings up to 40 at $1,500 each.
- Any booked meeting that doesn’t happen is added to your next summit, written into your sponsor agreement.
- Each summit is capped at 20 sponsors, each solving a different problem for the people in the room.
Want the category to yourself? Each summit is capped at 20 sponsors. To talk about your category, .
- Plant leaders ask to meet you. We seat the ones who asked at your table.
- Your booked meeting schedule arrives before the summit.
- Any booked meeting that doesn't happen is added to your next summit: miss 3, and you get 15 plus 3. It's written into your sponsor agreement.
- You get the delegate list 30 days before the summit: names, titles and companies.
- Three people are included with full access. Extra passes are $2,900 each.
Or pick only what you wantMeetings from $15,000, talk $15,000, exhibit $15,000, dining table $10,000
One category, one summit. Prices in USD. Whatever you pick includes three people with full access. Meetings are booked on an opt-in basis before the summit; any booked meeting that doesn't happen is added to your next summit.
No vendor walks the show. Solution providers attend only as sponsors. A vendor that has not sponsored cannot register, attend or work the room, so the plant leaders you meet are not being chased by your competitors in the hallway.
The ten questions every sponsor asks.
Past sponsors answer all ten in one 5-minute film. Pick a question and the film jumps to its answer.
Now ask your own questions.
Answered on camera by past FMA sponsors. Recorded at past FMA summits.
Who's behind it.
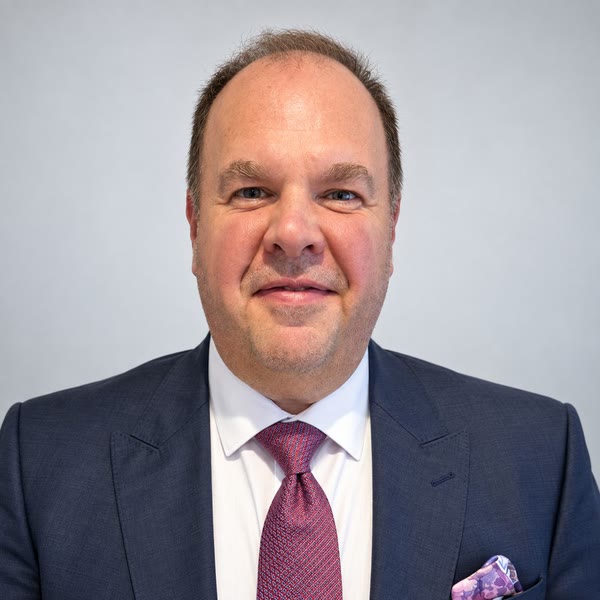
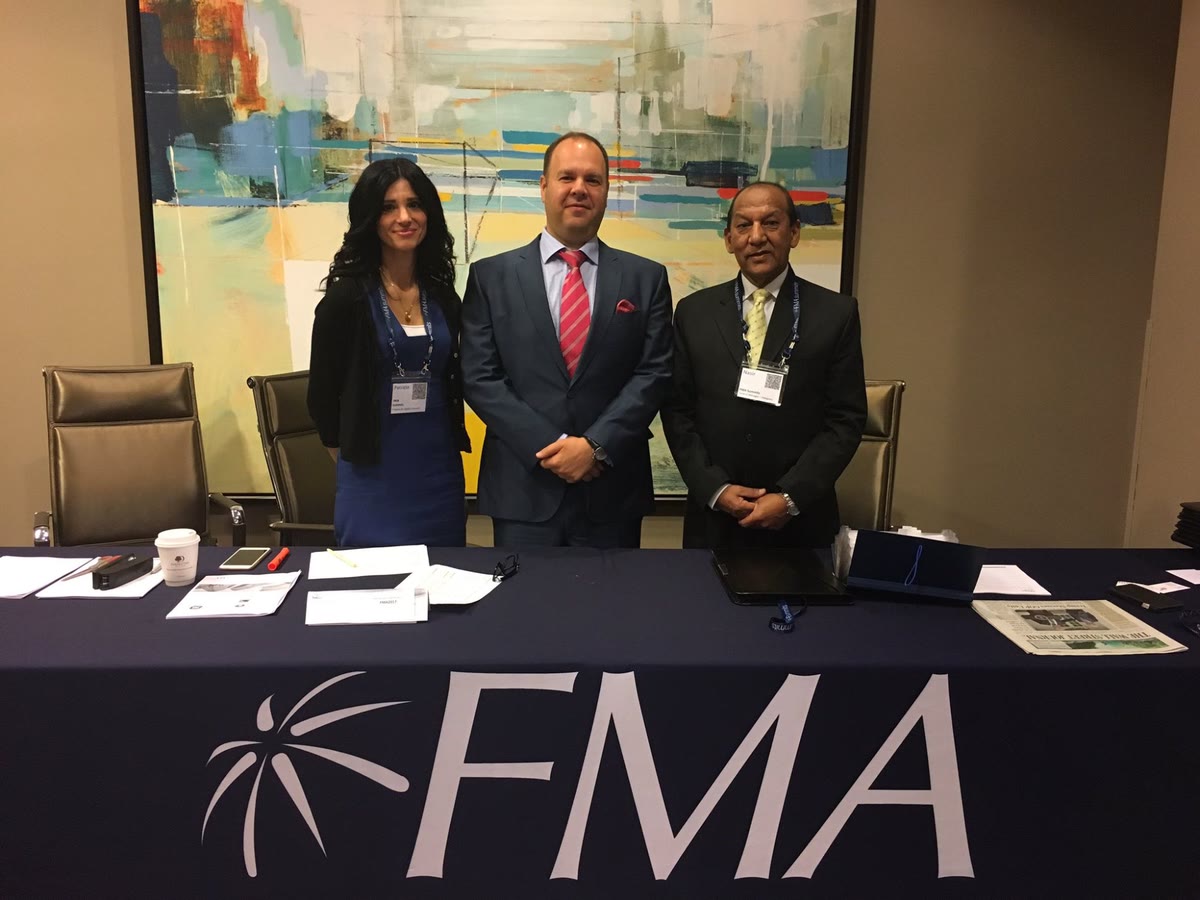
Started FMA in Montreal in 2007 and has run every summit himself: 35 of them, 17,000+ meetings. Capped at 20 sponsors per summit, meetings booked before anyone arrives, and no vendor walks the show.
Read the full story
30 printed programs, with every sponsor and speaker as printed.
Open any programCapped at 20 sponsors per summit. Your next customer already has a dust hazard analysis due.
Twenty minutes with Joe Piazza: who is coming to your summit, where your company fits among its 20 sponsors, and what the agreement says. The sponsor brief has the delegate profile, the full agenda and the itemized pricing.
35 summits since 2007. Joe Piazza, who founded FMA, runs every summit himself. The videos on this page are from past summits.